
There’s a configuration error that manufacturers in complex discrete categories see repeatedly, and it almost always traces back to the same moment: the point where a sales rep translates a customer conversation into a specification sheet.
The customer described what they needed. The rep wrote it down. The engineer read it. Three people interpreted the same requirement through three different mental models — and somewhere in that chain, a tolerance was wrong, a variant was misspecified, or an incompatible option combination made it through to the order.
In capital equipment, the cost of that error isn’t an exchange form. It’s a return freight bill, a production halt, a re-engineering cycle, and a customer relationship that now has a story attached to it.
3D CPQ is the architecture that closes that gap — not by making people more careful, but by making the error impossible to commit in the first place.
This is a technical and commercial breakdown of how it works, what the integration architecture looks like, and what manufacturers in the 2026 sales environment are actually building.
What 3D CPQ Actually Is — and What It Isn’t
Configure-Price-Quote software has existed for decades. The core concept is straightforward: a rules engine that constrains what a sales rep can configure based on the product’s engineering logic, and automatically prices the valid configuration before generating a quote document.
Traditional CPQ is largely a form-filling exercise. The rep works through a sequence of dropdown menus. The system validates selections against a rules table and calculates a price. The output is a quote document with a line-item specification table attached.
This works for simple products. For complex discrete manufacturing — industrial machinery, custom HVAC systems, modular process equipment, engineered-to-order enclosures, specialty vehicles — it breaks down at the point where the customer’s decision-making is most critical: visualization.
A customer configuring a £180,000 piece of processing equipment cannot meaningfully evaluate a specification table. They need to see the machine in the configuration they’re ordering — its physical footprint, its installation clearances, how the optional modules attach to the base unit, whether the material handling inlet will clear their existing ceiling height. A dropdown menu that says “Extended arm: Yes/No” doesn’t give them that.
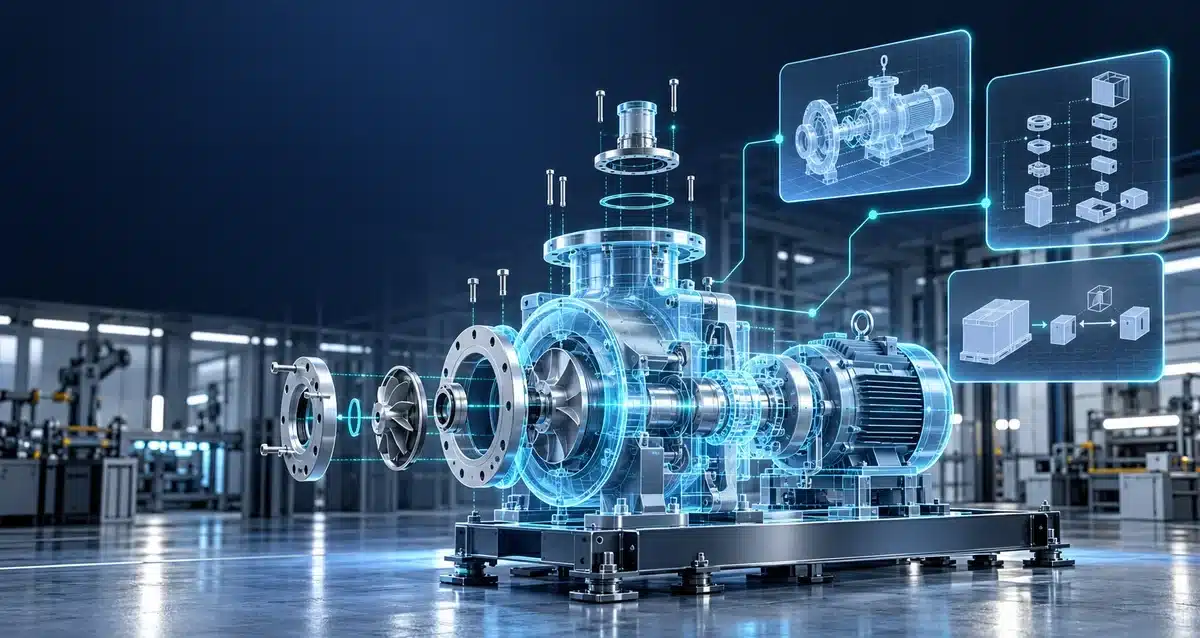
3D CPQ integrates a real-time 3D visualization engine directly into the configuration workflow. Every selection the customer or sales rep makes — dimensions, modules, finishes, optional components — drives an immediate update to a 3D model rendered in the browser. The model is geometrically accurate, not illustrative. The dimensions it shows are the dimensions that will be manufactured.
That’s the distinction that makes it commercially significant. It’s not a 3D product image attached to a quote. It’s a live parametric 3D model that reflects the exact configuration being ordered, at accurate scale, with accurate geometry.
Where Order Errors Actually Come From in Complex Manufacturing Sales
Before getting into the architecture, it’s worth being specific about the error vectors 3D CPQ addresses — because they’re not all in the same place.
Specification translation errors happen when a customer’s verbal or written requirement is interpreted by a sales rep who lacks the engineering depth to know that “slightly wider” has a specific meaning in that product family, or that the mounting configuration the customer described is incompatible with the motor size they also asked for. The rep can’t see the incompatibility because they’re working in text.
Variant combination errors happen when a valid-looking configuration is actually physically impossible. A longer conveyor bed with a certain drive unit requires a specific minimum clearance that a simultaneously-selected enclosure doesn’t provide. In a rules-table CPQ without 3D, this error may not surface until the CAD model is generated — weeks into the order process.
Customer expectation errors happen when the customer approves a specification table that doesn’t match what they thought they were ordering. They see “Module B — overhead” and approve it. What arrives is not what they pictured. The specification was correct. The communication was wrong.
Downstream BOM errors happen when a valid configuration generates an incorrect or incomplete bill of materials because the BOM generation logic wasn’t updated to reflect a recently-added variant or module combination.
3D CPQ addresses the first three directly — the visual layer eliminates specification translation errors and makes variant incompatibilities visible in real time. The automated BOM generation from confirmed configuration addresses the fourth.
The Integration Architecture: How 3D CPQ Connects to the Manufacturing Stack
This is where 3D CPQ becomes an infrastructure question rather than just a sales tool question. A properly architected 3D CPQ deployment connects four systems: the configuration engine, the 3D visualization layer, the ERP/BOM system, and the CAD system. Each integration point has specific technical requirements.
Layer 1: The Configuration Engine (Rules + Constraints)
The core of any CPQ deployment is the product rules engine — the logic that defines what combinations are valid and what combinations are physically impossible. In 3D CPQ, this rules engine needs to do more than validate dropdown selections. It needs to drive the parametric 3D model.
This means configuration rules need to be expressed in a form that both the business logic layer (pricing, quoting) and the 3D engine can consume. The practical architecture for this in 2026 is a constraint model maintained in a structured format (JSON or XML) that is read by both the rules engine and the 3D visualization layer simultaneously.
When a user selects a module, the constraint model: 1. Validates the selection against all other active selections 2. Eliminates incompatible options from subsequent menus (preventing the error before it can be made) 3. Triggers a geometry update in the 3D viewer that reflects the new module’s physical presence in the configuration
The critical design decision at this layer is whether to maintain the constraint model as a standalone artifact (maintainable by product engineers without CPQ vendor involvement) or to bake it into the CPQ platform’s proprietary rules engine. The former is significantly more maintainable as products evolve.
Layer 2: The 3D Visualization Engine
The 3D viewer in a manufacturing CPQ context has different requirements than a consumer product configurator. The priorities are:
Geometric accuracy over visual fidelity. The model needs to be dimensionally correct — the customer is using it to verify clearances and installation requirements, not to admire renders. Photorealistic rendering is useful but secondary.
Parametric, not asset-swap. Low-budget implementations use a library of pre-rendered 3D assets and swap them in and out as the user makes selections. This works for simple products with discrete visual states. For complex machinery with continuously variable dimensions (adjustable bed lengths, variable motor positions, telescoping components), you need a parametric model that recalculates geometry in real time based on input parameters.
Browser-native delivery. The 3D viewer needs to run in a standard browser without plugin installation. Manufacturers’ dealers and procurement teams won’t install proprietary viewers — and the configuration session often happens on a customer’s device in their facility. WebGL-based rendering is the standard approach in 2026; Three.js, Babylon.js, and proprietary WebGL engines are all viable depending on the geometry complexity.
Performance on real hardware. Complex parametric models can become GPU-intensive. The 3D layer needs to perform on a mid-range business laptop — not a workstation. Level-of-detail management and progressive loading are architectural requirements, not optional features.
Layer 3: Automated BOM Generation
This is where 3D CPQ generates its clearest ROI signal for manufacturing operations.
When a configuration is confirmed in the CPQ system, the confirmed parameter set is complete and unambiguous. Every option is specified. Every module is selected. Every dimension is locked. The BOM that needs to be generated from that configuration is deterministic — there is exactly one correct BOM for that configuration, and it can be computed without human interpretation.
The integration architecture for automated BOM generation connects the confirmed CPQ configuration to the ERP system (SAP, Oracle, Infor, or ERP-native BOM modules) via an API that maps configuration parameters to component codes. The mapping layer is typically maintained as a configuration matrix — a structured table that says “when Module B is selected with Drive Unit 3, add these three component codes to the BOM.”
The engineering work in building this layer is substantial, and it’s the part that most 3D CPQ implementations underestimate. The component mapping needs to be comprehensive — every valid configuration combination needs a defined BOM output. For a product family with 50 configurable parameters, each with 5–10 options, the combination space is large. The practical approach is to decompose this into sub-assemblies: each module or sub-system generates its own partial BOM, and the complete BOM is assembled from partial BOMs based on the full configuration.
The output of the automated BOM generation isn’t just a list of components. It includes: – Component quantities calculated from configured dimensions (material lengths, fastener counts) – Manufacturing instructions flagged by configuration variant (non-standard configurations requiring engineering sign-off) – Lead time signals pulled from the ERP’s inventory and procurement data – Pricing data fed back to the CPQ’s price calculation
Layer 4: CAD-to-Quote Automation
The most technically ambitious element of 3D CPQ architecture is closing the loop back to the CAD system — so that a confirmed configuration produces not just a quote document and a BOM, but a CAD file ready for the manufacturing floor.
The architecture for this varies significantly depending on the CAD environment. The two main approaches:
Parameter-driven CAD automation: The CAD system (SOLIDWORKS, Inventor, Creo, or equivalent) maintains master parametric models with named parameters for every configurable dimension and variant. When a configuration is confirmed in the CPQ system, a structured parameter file is passed to the CAD system via API (or file-based integration), and the CAD software regenerates the model with the confirmed parameters. The output is a fully validated CAD model in the standard format — ready for DXF/DWG extraction, tolerance checking, and routing to the manufacturing floor.
Geometry kernel integration: For manufacturers with highly variable product geometry (products that don’t map cleanly to a fixed parametric model), the alternative is to integrate a geometry kernel directly into the 3D CPQ layer — so the 3D model generated in the browser is the CAD geometry, not a visualization approximation of it. The confirmed model is then exported directly to the appropriate CAD format. This is more architecturally complex but eliminates the translation step between the visualization model and the manufacturing model.
The CAD-to-quote loop matters commercially because it compresses the time between order confirmation and manufacturing commencement. The traditional sequence — configuration approved, order placed, CAD model created, BOM generated, production scheduled — can run 2–6 weeks for complex products. With automated parameter-driven CAD output, the configuration-to-production-ready-model time drops to hours.
The 3D Sales Portal for B2B Dealers: A Different Architecture Problem
Many complex manufacturers don’t sell directly to end customers. They sell through dealer networks — regional distributors who may handle multiple product lines, whose sales teams have variable product knowledge, and who need to present configurations to end customers in their own branded environments.
The 3D CPQ architecture for dealer networks has a specific set of requirements that differ from a direct sales deployment:
Multi-tenancy with brand isolation. Each dealer needs their own branded configuration portal, but the underlying product rules, pricing engine, and 3D models should be maintained centrally by the manufacturer. Dealer branding is applied at the presentation layer; the product logic is not replicated per dealer.
Tiered pricing rules. Dealer pricing typically differs from end-customer pricing and from other dealers based on volume commitments, territory agreements, or product line certifications. The pricing layer needs to apply the correct price tier based on the authenticated dealer identity without exposing pricing logic to the dealer or end customer.
Dealer-controlled quote presentation. The dealer needs to be able to customise the quote document — adding their own branding, terms, and contact information — without modifying the underlying configuration specification. The architecture typically provides a quote template layer that the dealer can configure independently of the product configuration layer.
Offline capability for on-site demos. Industrial product sales often happen on-site at the customer’s facility, where internet connectivity may be limited. A dealer-facing 3D CPQ portal needs progressive web app architecture with offline-first data management — so a pre-loaded configuration can be demonstrated and modified without an active connection, with synchronisation when connectivity is restored.
Access-controlled product visibility. Dealers certified for certain product lines should not see products outside their certification. The product catalogue visibility layer needs to enforce access control based on dealer profile, not just authentication.
What Automated BOM Generation Changes for Manufacturing Operations
The operational impact of automated BOM generation extends beyond the order entry process. It changes the shape of the manufacturing operations team’s workload in ways that aggregate into substantial cost reduction.
Engineering-to-order labour reduction. In a traditional ETO workflow, every custom order requires an engineer to review the configuration, generate the BOM, and verify completeness before release to production. For manufacturers processing 50–200 custom orders per month, this is a significant engineering labour allocation. Automated BOM generation from confirmed configurations eliminates this for standard configurations and flags only genuinely non-standard combinations for engineering review.
Procurement lead time compression. When the BOM is generated at order confirmation — not 2–3 weeks later — long-lead components can be ordered earlier in the production cycle. For components with 8–12 week lead times, this compression directly affects manufacturing throughput capacity.
First-pass yield improvement. Orders that enter production with an accurate, complete BOM have higher first-pass yield rates than orders that were manually specified. The root cause is the same as the ordering error root cause: when humans translate specifications, they introduce error. When the BOM is generated deterministically from a confirmed configuration, it’s correct by construction.
Returns and rework cost reduction. The headline metric for 3D CPQ ROI in complex manufacturing is typically the reduction in post-delivery returns and specification disputes. Across implementations in industrial equipment categories, the range reported in the literature is 30–50% reduction in specification-related returns. The mechanism is direct: the customer confirmed a 3D model that accurately represented what was manufactured. There is no gap between expectation and delivery.
Implementation Sequence: How Manufacturers Are Actually Building This in 2026
The realistic implementation sequence for a manufacturer building 3D CPQ from a standing start is typically 12–18 months for a production-grade deployment. The phases:
Phase 1 (Months 1–3): Configuration model and rules definition. Before any 3D work begins, the product configuration logic needs to be formally specified. This is often the most revealing phase — it surfaces configuration rules that exist in engineers’ heads but have never been formally documented, and it identifies gaps in the constraint logic that have historically been caught by experienced reps rather than by the system. Output: a complete constraint model for the priority product family.
Phase 2 (Months 2–5): 3D model preparation. The parametric 3D models that will drive the visualization layer need to be prepared from the master CAD models. For most manufacturers, this means creating a “visualization model” that is geometrically accurate but optimised for browser rendering — reduced polygon count in areas of low visual importance, pre-baked texture maps for surface finishes, defined parameter hooks that the configuration engine will drive. This phase overlaps with Phase 1.
Phase 3 (Months 4–8): CPQ and 3D engine integration. The configuration engine and 3D viewer are integrated so that configuration changes drive real-time model updates. This is the core technical work of the project and the phase where the architecture decisions made in Phases 1–2 either pay off or create rework.
Phase 4 (Months 7–12): BOM and ERP integration. The automated BOM generation layer is built and validated. This phase requires close collaboration between the CPQ implementation team and the ERP team — mapping configuration parameters to component codes is a data exercise that requires both product knowledge and ERP expertise. Validation involves running confirmed configurations through the automated BOM path and comparing outputs against manually-generated BOMs for equivalence.
Phase 5 (Months 10–18): Dealer portal and CAD automation. The dealer-facing portal layer is deployed, and the CAD automation integration is built for the priority product family. These phases can run in parallel; they share no dependencies.
The Commercial Case: What the Numbers Look Like
The ROI model for 3D CPQ in complex manufacturing is built from three distinct value streams, and they compound:
Order error reduction. A manufacturer processing 120 custom orders per month with a 4% specification error rate (a conservative estimate for complex products without CPQ) has roughly 5 problem orders per month. If each problem order costs an average of $15,000 to resolve (engineering investigation, production disruption, re-manufacture or rework, return logistics), that’s $75,000 per month in error costs. A 40% reduction in error rate saves $30,000 per month, or $360,000 per year.
Sales cycle compression. When a customer can configure, visualise, and approve in a single session — rather than a sequence of back-and-forth involving engineering reviews and revised specifications — the sales cycle shortens. For complex industrial products with typical cycles of 3–9 months, compressing the configuration-to-approval phase by 3–6 weeks doesn’t just improve cash flow forecasting. It increases the number of deals that can be active simultaneously with the same sales team.
Engineering labour reallocation. Engineers currently performing manual BOM generation and order validation for standard configurations can be reallocated to genuinely non-standard applications and product development. For a manufacturing firm employing 4–6 engineers whose time is partially consumed by routine order processing, this reallocation represents significant capacity for higher-value work.
The investment to deploy a production-grade 3D CPQ system for a complex manufacturer — including 3D model preparation, integration development, and dealer portal — typically runs $150,000–$400,000 depending on product complexity, the number of product families in scope, and the depth of ERP integration. Against the value streams above, payback periods of 12–24 months are common. For manufacturers with high order volumes and high error costs, payback under 12 months is achievable.
What to Evaluate When Selecting a 3D CPQ Implementation Partner
The market for 3D CPQ implementation is less standardised than the market for standard CPQ, and the technical requirements are more demanding. Several things to evaluate rigorously:
Parametric modelling capability, not asset swap. Ask the partner to demonstrate the system with a product that has continuously variable dimensions. If the demo shows fixed 3D assets being swapped, the architecture won’t scale to your product’s complexity.
ERP integration depth. Ask specifically about BOM generation automation and what the mapping layer looks like. A partner who describes this as “straightforward” without being able to show you the mapping architecture probably hasn’t built it before.
Browser performance on representative hardware. Test the system on a standard business laptop, not a workstation. The demo environment is not the customer environment.
CAD system integration. If automated CAD output is a requirement, verify that the partner has delivered this integration for your specific CAD platform. SOLIDWORKS, Inventor, and Creo have different API surfaces; experience with one doesn’t transfer directly to another.
Maintenance model for configuration rules. Ask who maintains the constraint model as the product evolves. If the answer is “you submit a change request to us,” you have a dependency on the vendor for every product update. If the answer is “your product engineers maintain it in a structured format we’ve documented,” you have a sustainable operational model.
The Competitive Pressure Making This Urgent
The case for 3D CPQ doesn’t rest purely on internal efficiency gains. There’s a competitive dimension that’s becoming relevant in 2026 for complex manufacturers.
Enterprise procurement teams are increasingly expecting configuration experiences that match the quality of consumer digital experiences. A procurement manager who configured their home renovation in a browser-based tool last weekend has a calibration point for what “good” looks like in a configuration interface. A spreadsheet-based specification form followed by a two-week wait for a revised quote is not competing well against that reference point.
More directly: manufacturers in complex discrete categories who have deployed 3D CPQ are using it as a sales capability differentiator. When a prospect can configure, visualise, and receive an indicative quote in a single 40-minute session with your sales team — and your competitor requires three rounds of specification, an engineering review, and a six-week quote cycle — the competitive signal is clear.
The firms that establish 3D CPQ capability in 2025 and 2026 are setting the configuration experience standard in their categories. Industrial procurement teams who go through the process once have a new benchmark. Catching up from second place is harder than it looks.
Build This the Right Way the First Time
Ink N Algorithm works with manufacturers in complex discrete categories to design, specify, and deliver 3D CPQ deployments that connect the full stack — configuration engine, parametric 3D visualisation, automated BOM generation, ERP integration, and dealer portal architecture.
We start with a technical architecture review: your product’s configuration complexity, your current sales and ERP stack, and the specific error vectors costing you the most. The outcome of that review is a clear implementation roadmap with phasing, integration dependencies, and a realistic commercial case.
If your sales operations team is still resolving specification errors downstream, and your engineering team is still manually generating BOMs from hand-specified orders, the architecture to fix that is proven and deployable. The question is how quickly you move.
Talk to Ink & Algorithm about your 3D CPQ architecture →
Ink N Algorithm specialises in interactive 3D sales technology, CPQ integration architecture, and web-based configurator development for complex discrete manufacturers. Implementation metrics referenced in this article reflect live deployment data and published industry research.