
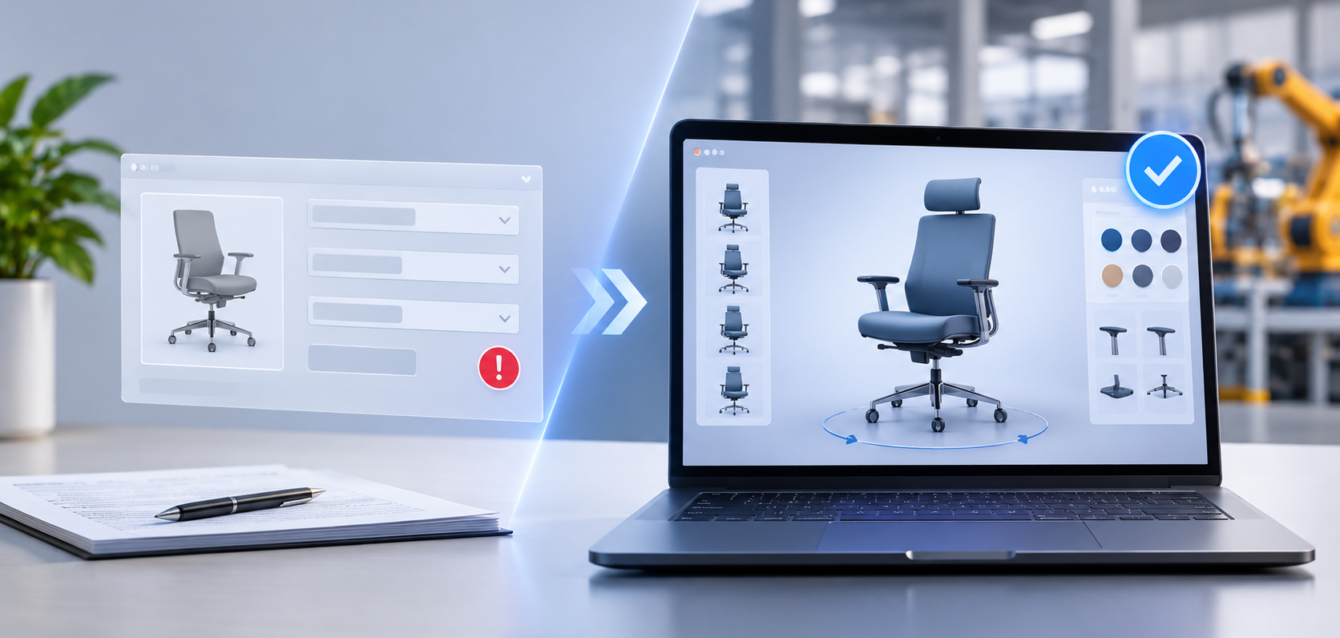
The 15% to 25% order error rate in complex manufacturing is not a people problem. It is an interface problem.
When a dealer or inside sales rep configures a modular product through a dropdown-based CPQ system — selecting from lists of part numbers, checking compatibility tables in a separate window, manually cross-referencing spec sheets for dimension constraints — the probability of an invalid configuration entering the sales order is not a function of their competence. It is a function of the system design. Text-based CPQ delegates the enforcement of physical constraints to human memory and manual verification. At any meaningful configuration complexity, that delegation fails at a predictable rate.
The commercial consequence is not abstract. In modular equipment manufacturing, a production order built on an invalid configuration means rework, re-scheduling, component substitution, and customer communication — typically at a fully-loaded cost of $2,000–$12,000 per corrected order, before accounting for the relationship damage of a delayed or mis-built delivery. At a production volume of 50–100 units per month with a 15% error rate, this is a $1.5M–$7.2M annual problem hiding in the ops budget under “rework” and “engineering change orders.”
3D parametric CPQ eliminates this class of error at the architectural level, not through better training or more careful process — through making invalid configurations mechanically impossible to submit.
Section 1: The Flaw in Traditional Text-Based CPQ
How Dropdown Logic Fails at Configuration Complexity
Traditional CPQ systems — whether purpose-built platforms like Salesforce CPQ, Oracle CPQ, or Tacton, or the spreadsheet-based configurators that dominate mid-market manufacturing — share a fundamental architectural assumption: that configuration validity can be enforced through cascading dropdown logic.
The cascading dropdown model works at low complexity. If a product has three option dimensions with five values each, 125 possible combinations, and a small set of exclusion rules, a well-maintained dropdown tree can enforce those rules adequately.
It fails at the complexity level that characterises actual discrete manufacturing products:
Geometric interdependencies: A modular conveyor system’s motor mount position depends on the frame width, which depends on the belt specification, which is constrained by the load rating, which affects the leg height. These are not logical rules — they are physical relationships that exist in three-dimensional space. A dropdown system must translate these relationships into conditional logic. That translation is incomplete by definition: it captures the rules the configuration team thought to encode, not the full set of physical constraints the assembly must satisfy.
Part number proliferation: A mid-complexity industrial product can have 50,000–500,000 valid configuration combinations. Maintaining accurate cascading dropdown constraints across this space requires constant synchronisation between the CPQ rules database and engineering change orders. In practice, the CPQ rules database is always at least one product revision behind. The delta is where invalid configurations enter.
The double-entry problem: In most text-based CPQ deployments, the sales rep enters the configuration in the CPQ system and the resulting order is re-entered by an order management or engineering team into the ERP or CAD system. Every re-entry step is an error introduction point. Manual transcription of part numbers, dimensions, and option codes from a CPQ quote document into an ERP production order is not a rare failure mode — it is the dominant source of manufacturing errors in the traditional CPQ workflow.
The 15–25% Quote Error Rate in Context
Industry benchmarks for configurable product manufacturing consistently show quote error rates in the 15–25% range for text-based CPQ deployments — meaning 15–25% of sales orders require at least one correction between order entry and production completion. The Aberdeen Group’s manufacturing CPQ research places the average cost of a single configurable-product order error at $4,700 when accounting for rework, re-scheduling, expediting, and customer communication.
At 100 units per month with a 20% error rate and $4,700 average error cost: $940,000 in annual error costs. For a business doing $15M–$40M in annual revenue, this is a material drag on margin that text-based CPQ cannot address at its root.
Parametric Rules Engine Architecture
Making Invalid Configurations Mechanically Impossible
A 3D parametric CPQ system does not translate physical constraints into dropdown logic. It encodes them directly into the 3D model’s parametric geometry — so the 3D model itself enforces the constraints, in the same way the physical assembly would.
The architecture has three layers:
Layer 1: Parametric 3D Model
The product’s 3D geometry is built as a parametric model, not a static mesh. Each component has parameters — dimensions, positions, attachment points — that are defined as functions of other parameters rather than as fixed values. When a buyer selects a wider frame, the model’s beam lengths, mounting hole positions, and clearance zones update automatically, because they are defined as functions of the frame width parameter.
This is the same parametric modelling approach used in CAD systems (SolidWorks, PTC Creo, Autodesk Inventor) — but delivered as an interactive web application rather than a desktop engineering tool. The browser-based 3D configurator runs the parametric engine client-side (WebGPU/WebGL) or server-side (via a compute session), and the buyer sees the product update in real time as they make selections.
Layer 2: Constraint Graph
Above the parametric geometry layer sits a constraint graph — a formal representation of the dependency relationships between configuration choices. The constraint graph is not a list of “if A then not B” rules; it is a directed graph where each node is a configuration parameter and each edge is a constraint relationship (equality, inequality, range, or derived function).
When a buyer selects a value for one parameter, the constraint graph propagates that choice through its dependency relationships, automatically resolving valid ranges for all dependent parameters. Options that would result in an invalid configuration are not presented as unavailable choices — they are not presented at all, because the constraint graph has already determined that they cannot coexist with the current parameter state.
The practical result: a buyer cannot construct an invalid configuration, not because they are warned away from it, but because invalid options do not appear in the interface when they would be invalid.
Layer 3: Rules Engine API
The constraint graph is served by a rules engine API — a backend service that holds the authoritative constraint data and evaluates configuration states against it. The browser-side configurator queries the rules engine on each parameter change, receives the updated valid option set, and updates the UI accordingly.
Separating the rules engine from the browser client is architecturally significant: it means the constraint data is maintained in one place, updated when product revisions occur, and queried by all channels — the web configurator, the dealer portal, the sales rep tool, and the ERP order entry interface. When engineering releases a product revision that changes a constraint, the update propagates to all channels simultaneously, because they all query the same rules engine.
Automated Bill of Materials Generation
From Configuration State to Production-Ready BOM in Real Time
Every parametric selection a buyer makes in a 3D CPQ system is a data event that updates the configuration state object. At any point in the configuration process, the configuration state is a complete, machine-readable description of the product being built.
The BOM generation engine reads the configuration state and produces a structured bill of materials — a list of every component, sub-assembly, fastener, and raw material required to build the configured product, with part numbers, quantities, and unit costs — in real time, updating as the buyer configures.
This is not a static BOM template with variable fields filled in. It is a dynamic computation: the parametric model’s component list is a function of the configuration parameters, so as the buyer changes dimensions or option selections, the BOM updates to reflect the components that the new configuration actually requires.
BOM Structure and ERP Compatibility
A production-ready BOM for ERP consumption has a defined structure. The 3D CPQ system generates BOM output in a format compatible with the target ERP system:
{ “bom_id”: “CFG-2026-11-04-A47F”, “product”: “modular_conveyor_mk4”, “configuration_hash”: “a3f7c291”, “line_items”: [ { “level”: 1, “part_number”: “FRM-2400-SS”, “description”: “Main Frame Assembly, 2400mm, Stainless”, “qty”: 1, “unit_cost”: 1240.00 }, { “level”: 2, “part_number”: “BLT-900-FDA”, “description”: “FDA-Grade Belt, 900mm width”, “qty”: 2.4, “unit”: “metres”, “unit_cost”: 48.50 }, { “level”: 2, “part_number”: “MTR-2200-IE3”, “description”: “Drive Motor, 2.2kW, IE3 Efficiency”, “qty”: 1, “unit_cost”: 680.00 } ], “total_material_cost”: 4820.00, “configuration_price”: 8750.00, “margin”: 0.449, “timestamp”: “2026-11-04T15:23:07Z”}
The configuration_hash is a compact identifier for the exact configuration state — it allows the ERP system to verify that the production order it receives matches the configuration the buyer approved, without transmitting the full configuration object in every API call.
Localised Pricing and Dealer Margin Layers
For businesses selling through dealer networks or across multiple geographic markets, the BOM generation engine applies pricing layers on top of the base material cost:
- Dealer tier pricing: The dealer’s contracted margin structure is applied at BOM generation time, so the dealer sees their net price and the buyer sees the retail price in the same interface, with no manual calculation required.
- Regional cost adjustments: Freight, duty, and local distribution costs can be parameterised by buyer location and applied automatically at the pricing layer.
- Lead-time premiums: Components with constrained availability in the current production window can carry a premium that is applied automatically when that component appears in the BOM.
The result: the price the buyer sees in the 3D configurator is the price the dealer will invoice, which is the price that will appear on the production order, which is the price that will be recorded in the ERP system. Price discrepancies between the quote and the order — a persistent source of post-sale disputes in traditional CPQ — are eliminated architecturally.
ERP & CRM Bidirectional Synchronisation
Passing Real-Time CAD Dimensions and Price Hashes into Enterprise Systems
The 3D CPQ system’s output is not a PDF quote document. It is a structured data payload that enterprise systems can consume directly — eliminating manual re-entry at every stage of the order lifecycle.
Salesforce CPQ Integration
Salesforce CPQ receives the configuration as a Quote Line Group, with each BOM line item mapped to a Product Line Item in Salesforce’s data model. The integration:
- Creates or updates the Opportunity in Salesforce with the configuration data
- Generates a Salesforce CPQ Quote with line items pre-populated from the BOM
- Attaches the 3D-rendered configuration image and PDF spec sheet to the Quote record
- Triggers the configured approval workflow (manager sign-off for orders above a price threshold)
The bidirectional component: when the sales rep modifies the Quote in Salesforce (adjusting a margin, changing a quantity, applying a discount), the change is pushed back to the 3D CPQ system, which validates the modification against the constraint graph. If the sales rep’s modification would create an invalid configuration, the CPQ system flags it before the Quote is sent to the customer — not after the order enters production.
HubSpot CRM Integration
For businesses on HubSpot, the integration creates a Deal with custom properties carrying the configuration ID, BOM total, and configuration price. HubSpot workflow automation assigns the deal to the appropriate rep, generates a task for quote review, and sends the buyer an automated confirmation email with their configuration summary and next steps.
The configuration summary email contains a shareable configuration link — a URL that opens the 3D CPQ system with the buyer’s exact configuration pre-loaded. The buyer can share it with colleagues, return to it later, or submit it as an order directly.
ERP Order Entry (NetSuite, SAP B1, Acumatica)
When the buyer or rep approves the quote, the ERP integration fires a webhook that creates a draft Sales Order in the ERP system with:
- BOM line items as Sales Order line items, with part numbers, quantities, and unit costs
- CAD-derived dimensions as custom order fields (used by production planning to schedule cutting, forming, and assembly operations)
- Configuration hash as an order reference field (allows production to verify the order against the original configuration at any stage)
- Lead-time calculation based on current component availability, returned from the ERP to the CPQ system and surfaced to the buyer before they confirm the order
The bidirectionality is the critical architectural feature. The ERP does not receive a one-way data push — it participates in the configuration process by providing real-time availability and lead-time data that the CPQ system surfaces to the buyer. A buyer configuring a product sees not just a price but a delivery date — computed from the actual availability state of the BOM components in the ERP’s inventory.
The 60% Sales Cycle Acceleration
How Visual Self-Service Eliminates the Engineering Bottleneck
The traditional CPQ sales cycle in complex manufacturing has a structural bottleneck: engineering review. Before a configuration can be quoted to a customer, an engineer must review it to confirm that it is buildable, that the specified components will fit and function together, and that the stated dimensions are achievable. For a team of five engineers reviewing 80 configurations per month, this review is typically a 2–5 day process per configuration — and it cannot be parallelised beyond the engineering team’s capacity.
3D parametric CPQ eliminates this bottleneck because the parametric rules engine has already performed the engineering review in real time. By the time a buyer submits a configuration, it has been validated against every geometric constraint, every compatibility rule, and every BOM feasibility check that the engineering team would otherwise apply manually. The engineering review becomes a spot-check, not a gate.
The sales cycle impact of removing this gate is consistent across deployments:
Quote turnaround: From 3–7 business days (traditional CPQ with engineering review) to same-day, frequently real-time for simpler configurations. Buyers who can receive a valid, priced quote in a self-service session convert at significantly higher rates than those who must wait for a quote to be prepared.
Dealer channel velocity: For businesses selling through dealer networks, 3D parametric CPQ enables dealers to generate valid, priced quotes independently — without submitting a configuration request to the manufacturer’s inside sales or engineering team. A dealer with a customer in front of them can close a configuration, generate a quote, and submit an order in a single session. The manufacturer’s team reviews completed orders, not configuration requests.
Engineering headcount reallocation: When engineering review is no longer a gate in the sales cycle, the engineering team’s capacity — previously consumed by CPQ validation — becomes available for product development, process improvement, and customer escalation handling. Companies that deploy 3D parametric CPQ consistently report that engineering headcount previously allocated to quote validation is reallocated to higher-value engineering work within 90 days of deployment.
Measured Outcomes
Across industrial CPQ deployments in the modular equipment, custom fabrication, and specialty vehicle categories, the consistent measured outcomes are:
- Quote error rate reduction: 15–25% (traditional CPQ) → 1–3% (3D parametric CPQ). The residual 1–3% represents errors introduced in post-quote manual steps, not in the configuration process itself.
- Sales cycle compression: 25–60% reduction in time from first inquiry to signed order, driven primarily by the elimination of the engineering review gate and the quote-revision cycle.
- Configuration session conversion: Buyers who reach a priced quote in a self-service 3D CPQ session convert to signed orders at 3–5× the rate of buyers who receive a quote document via email after a manual process.
- Average deal size increase: Visual parametric configurators consistently produce higher average order values than text-based CPQ, because buyers discover and select options they would not have considered in a dropdown interface — driven by seeing their effect on the product in real time.
Ink & Algorithm’s 3D CPQ Practice
Ink & Algorithm designs and builds parametric 3D CPQ systems for complex discrete manufacturing, modular equipment, and industrial product companies — integrating real-time constraint enforcement, automated BOM generation, and bidirectional ERP/CRM synchronisation into a browser-delivered configurator that runs without app installation on any device.
For VP Sales Operations and CIO-level teams evaluating CPQ architecture, we provide a scoped technical assessment: analysis of your product’s configuration complexity, your current CPQ error rate, and your ERP/CRM stack — with a documented architecture proposal and ROI model before any development commitment.